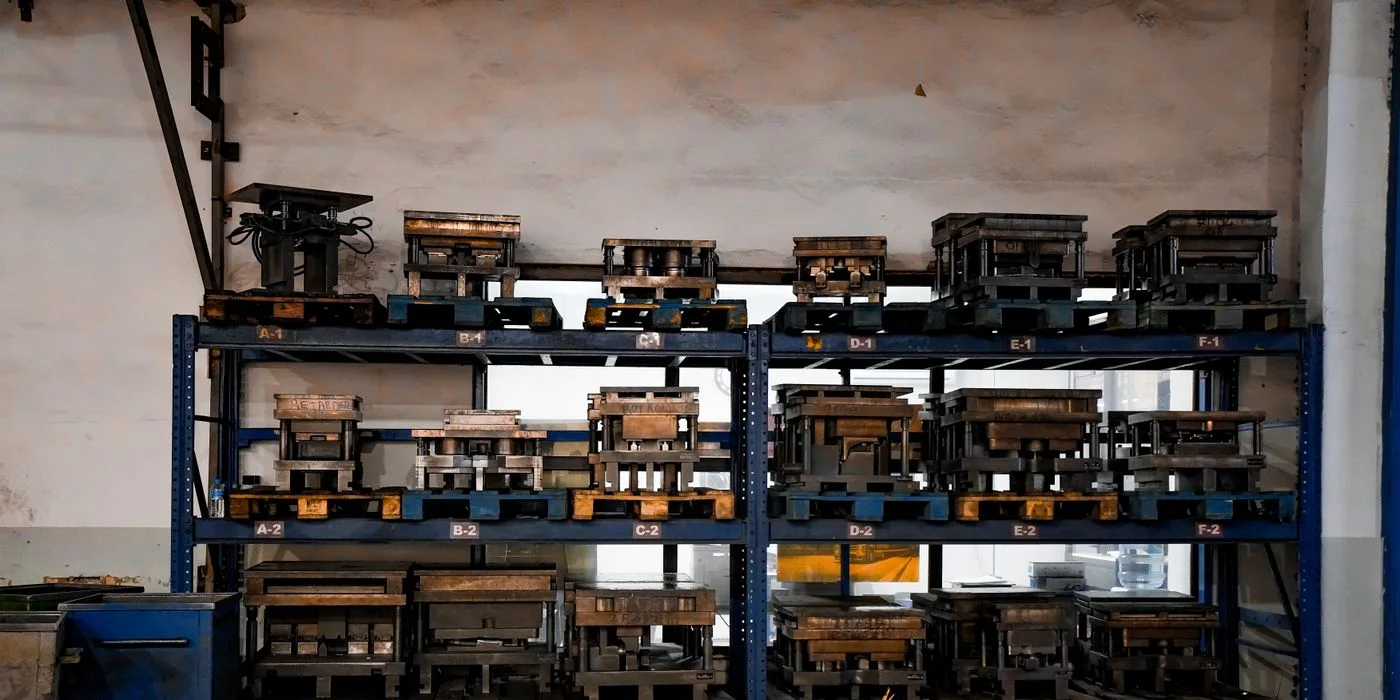
Two presses stand idle on opposite sides of the plant. Each can run Monday's jobs, but both jobs require the same qualified die. A schedule that books machine hours alone overlooks the real capacity limit.
Plot the tool as its own resource
Order A needs the die from 08:00 to 11:00. Order B is due to start at 10:30 on the other press. Even with zero transfer time, the assignments overlap by 30 minutes. If removal, transfer and installation need 40 minutes under the site's plan, the earliest feasible start on the second press is 11:40. Confirm the assumption with the responsible team.
Give planning a usable alternative
The planner can move B, resequence the jobs or verify that another qualified die is actually available. Identify the exact tool and its release status before committing to the alternative. The Manufacturing360 planning stage checks tooling alongside material and line capacity. Record the selected sequence against the orders so each supervisor knows which job releases the shared tool next.
More to discover in Numerish.
Explore related insights and practical enterprise workflows.